Motor Driven Roller
From Processing to Secondary Packaging
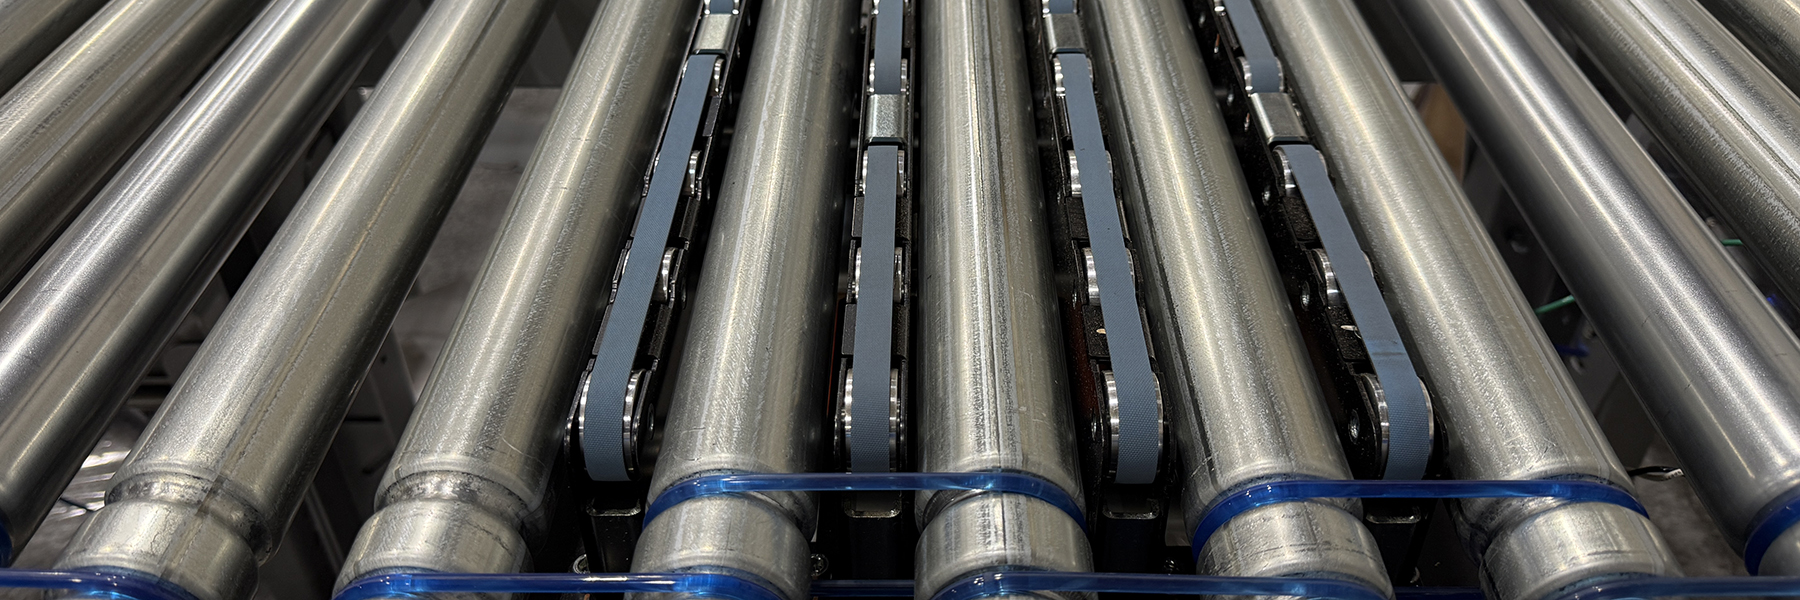
Nercon’s Motor Driven Roller (MDR) solutions expand capabilities to cover everything from processing through secondary packaging.
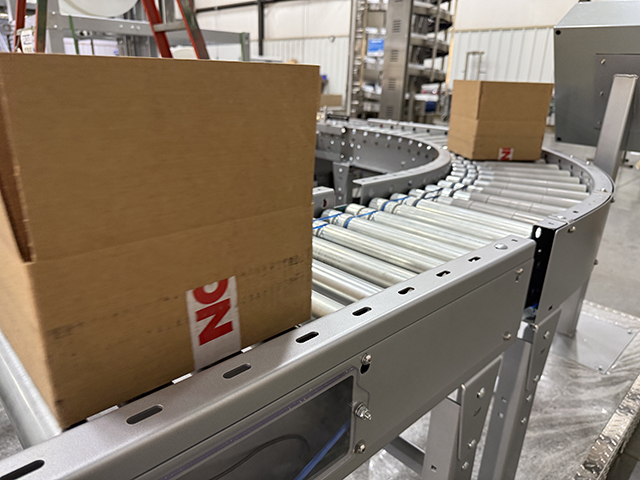
Taking an industry standard and integrating it with Nercon's reliable design and engineering.
Expanded Solutions
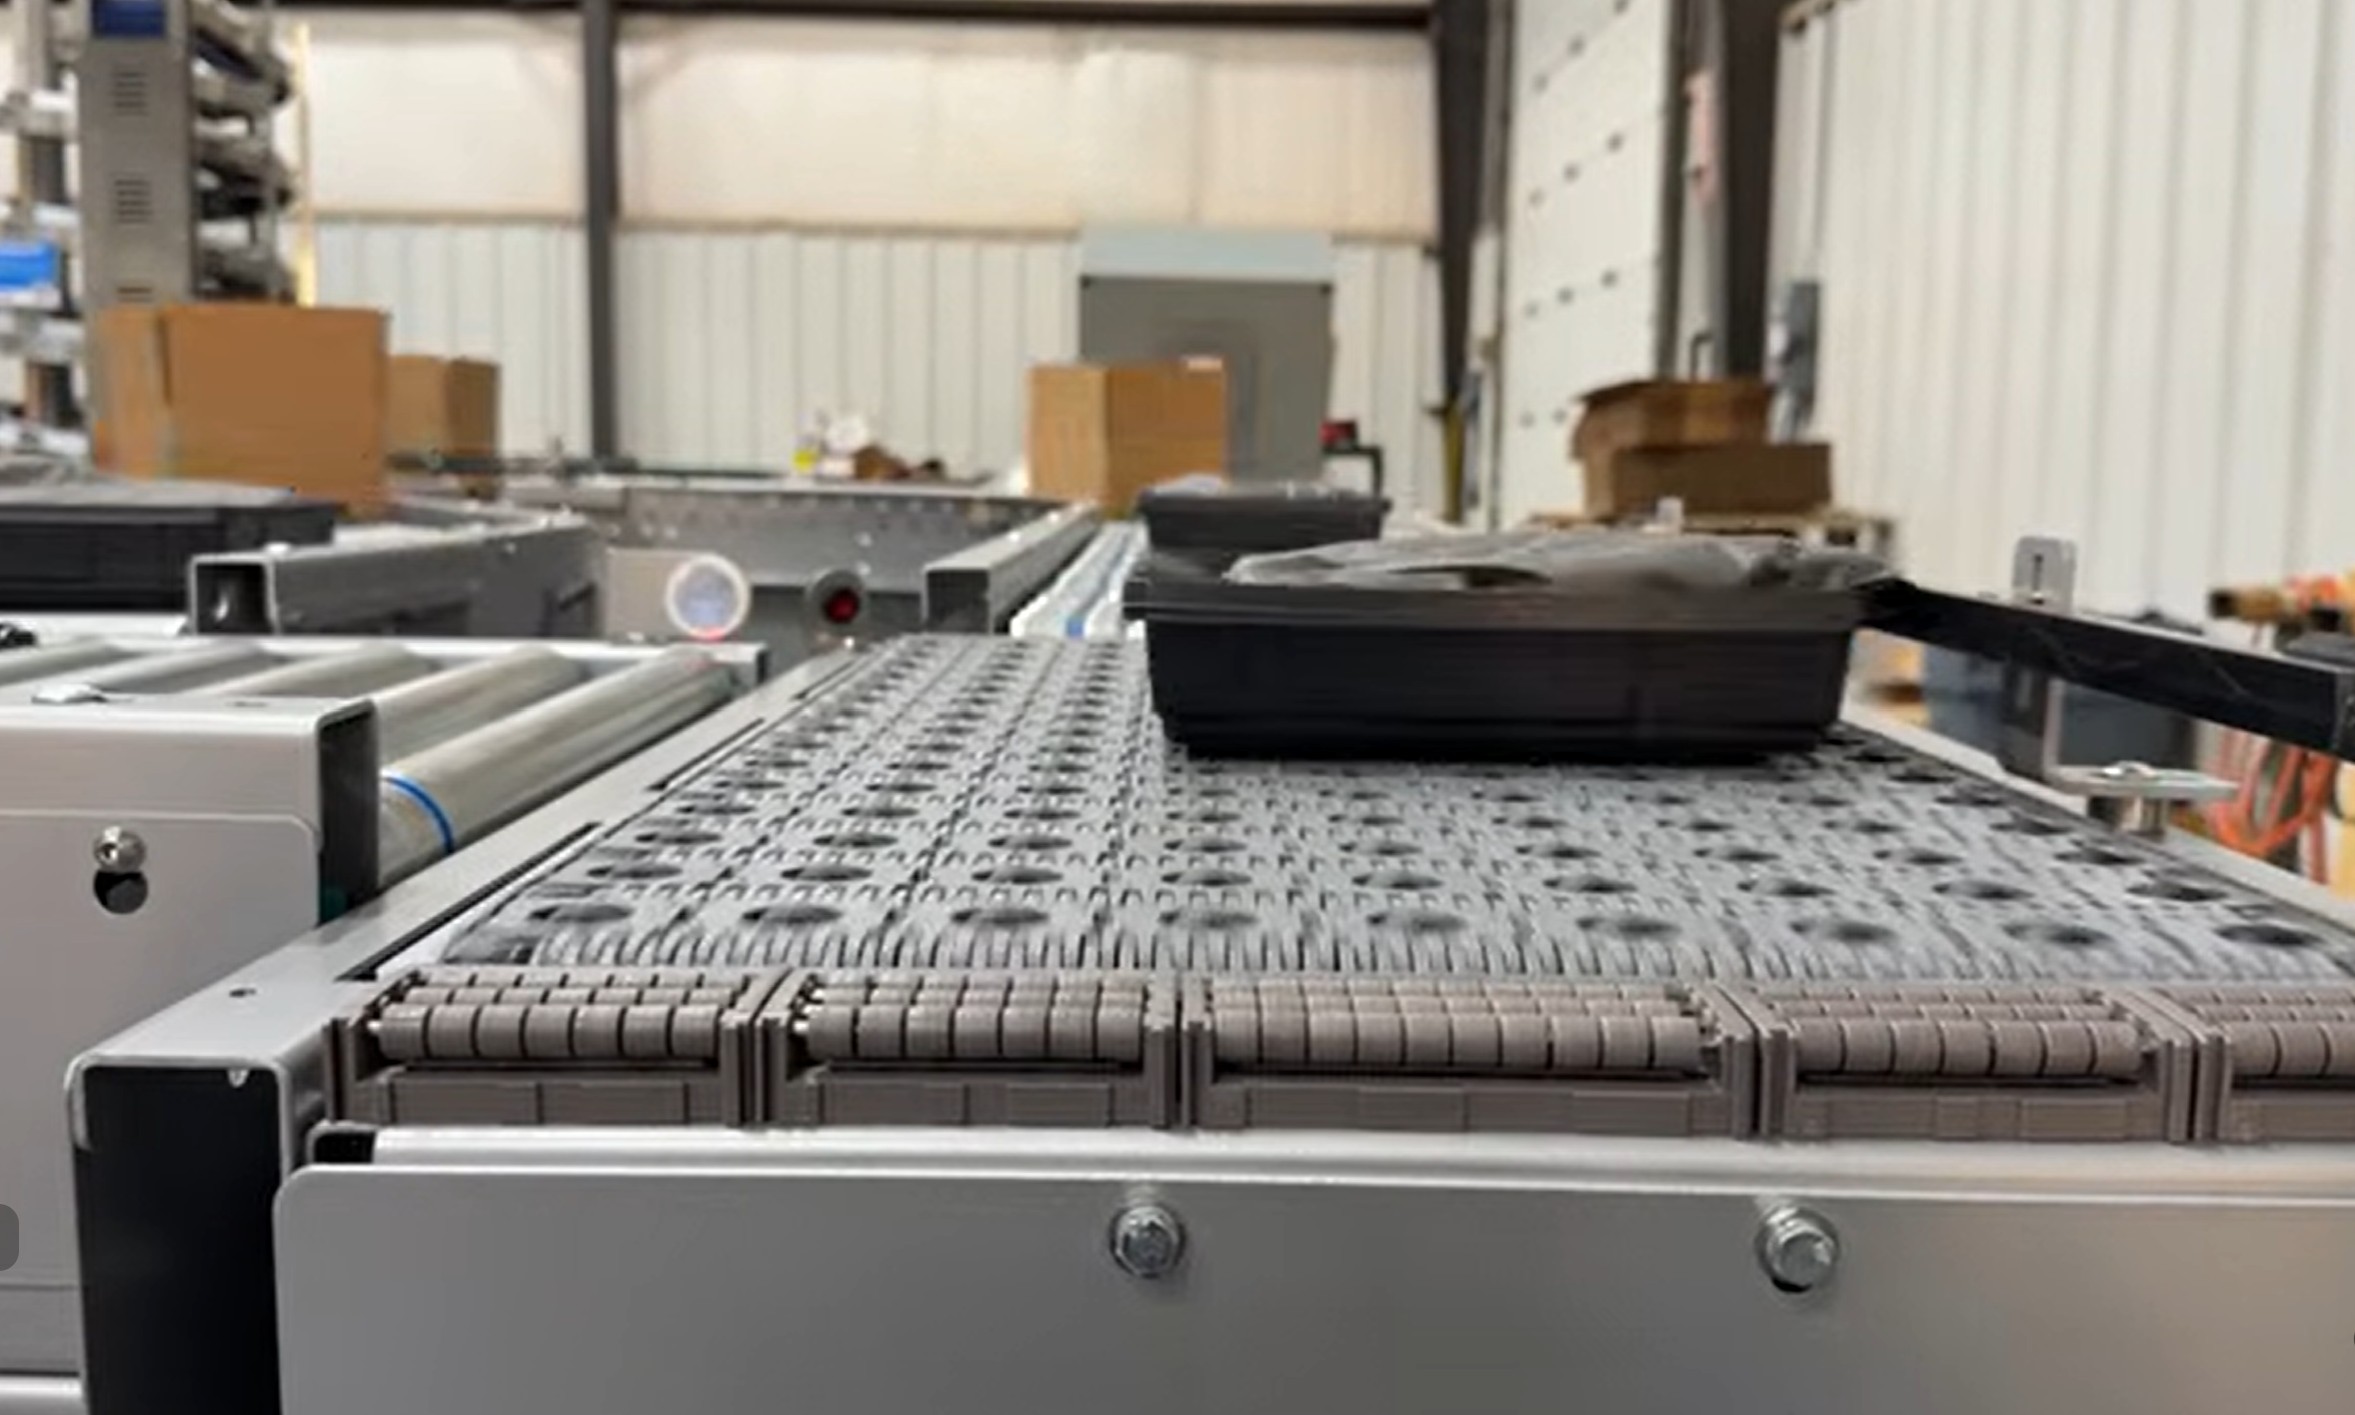
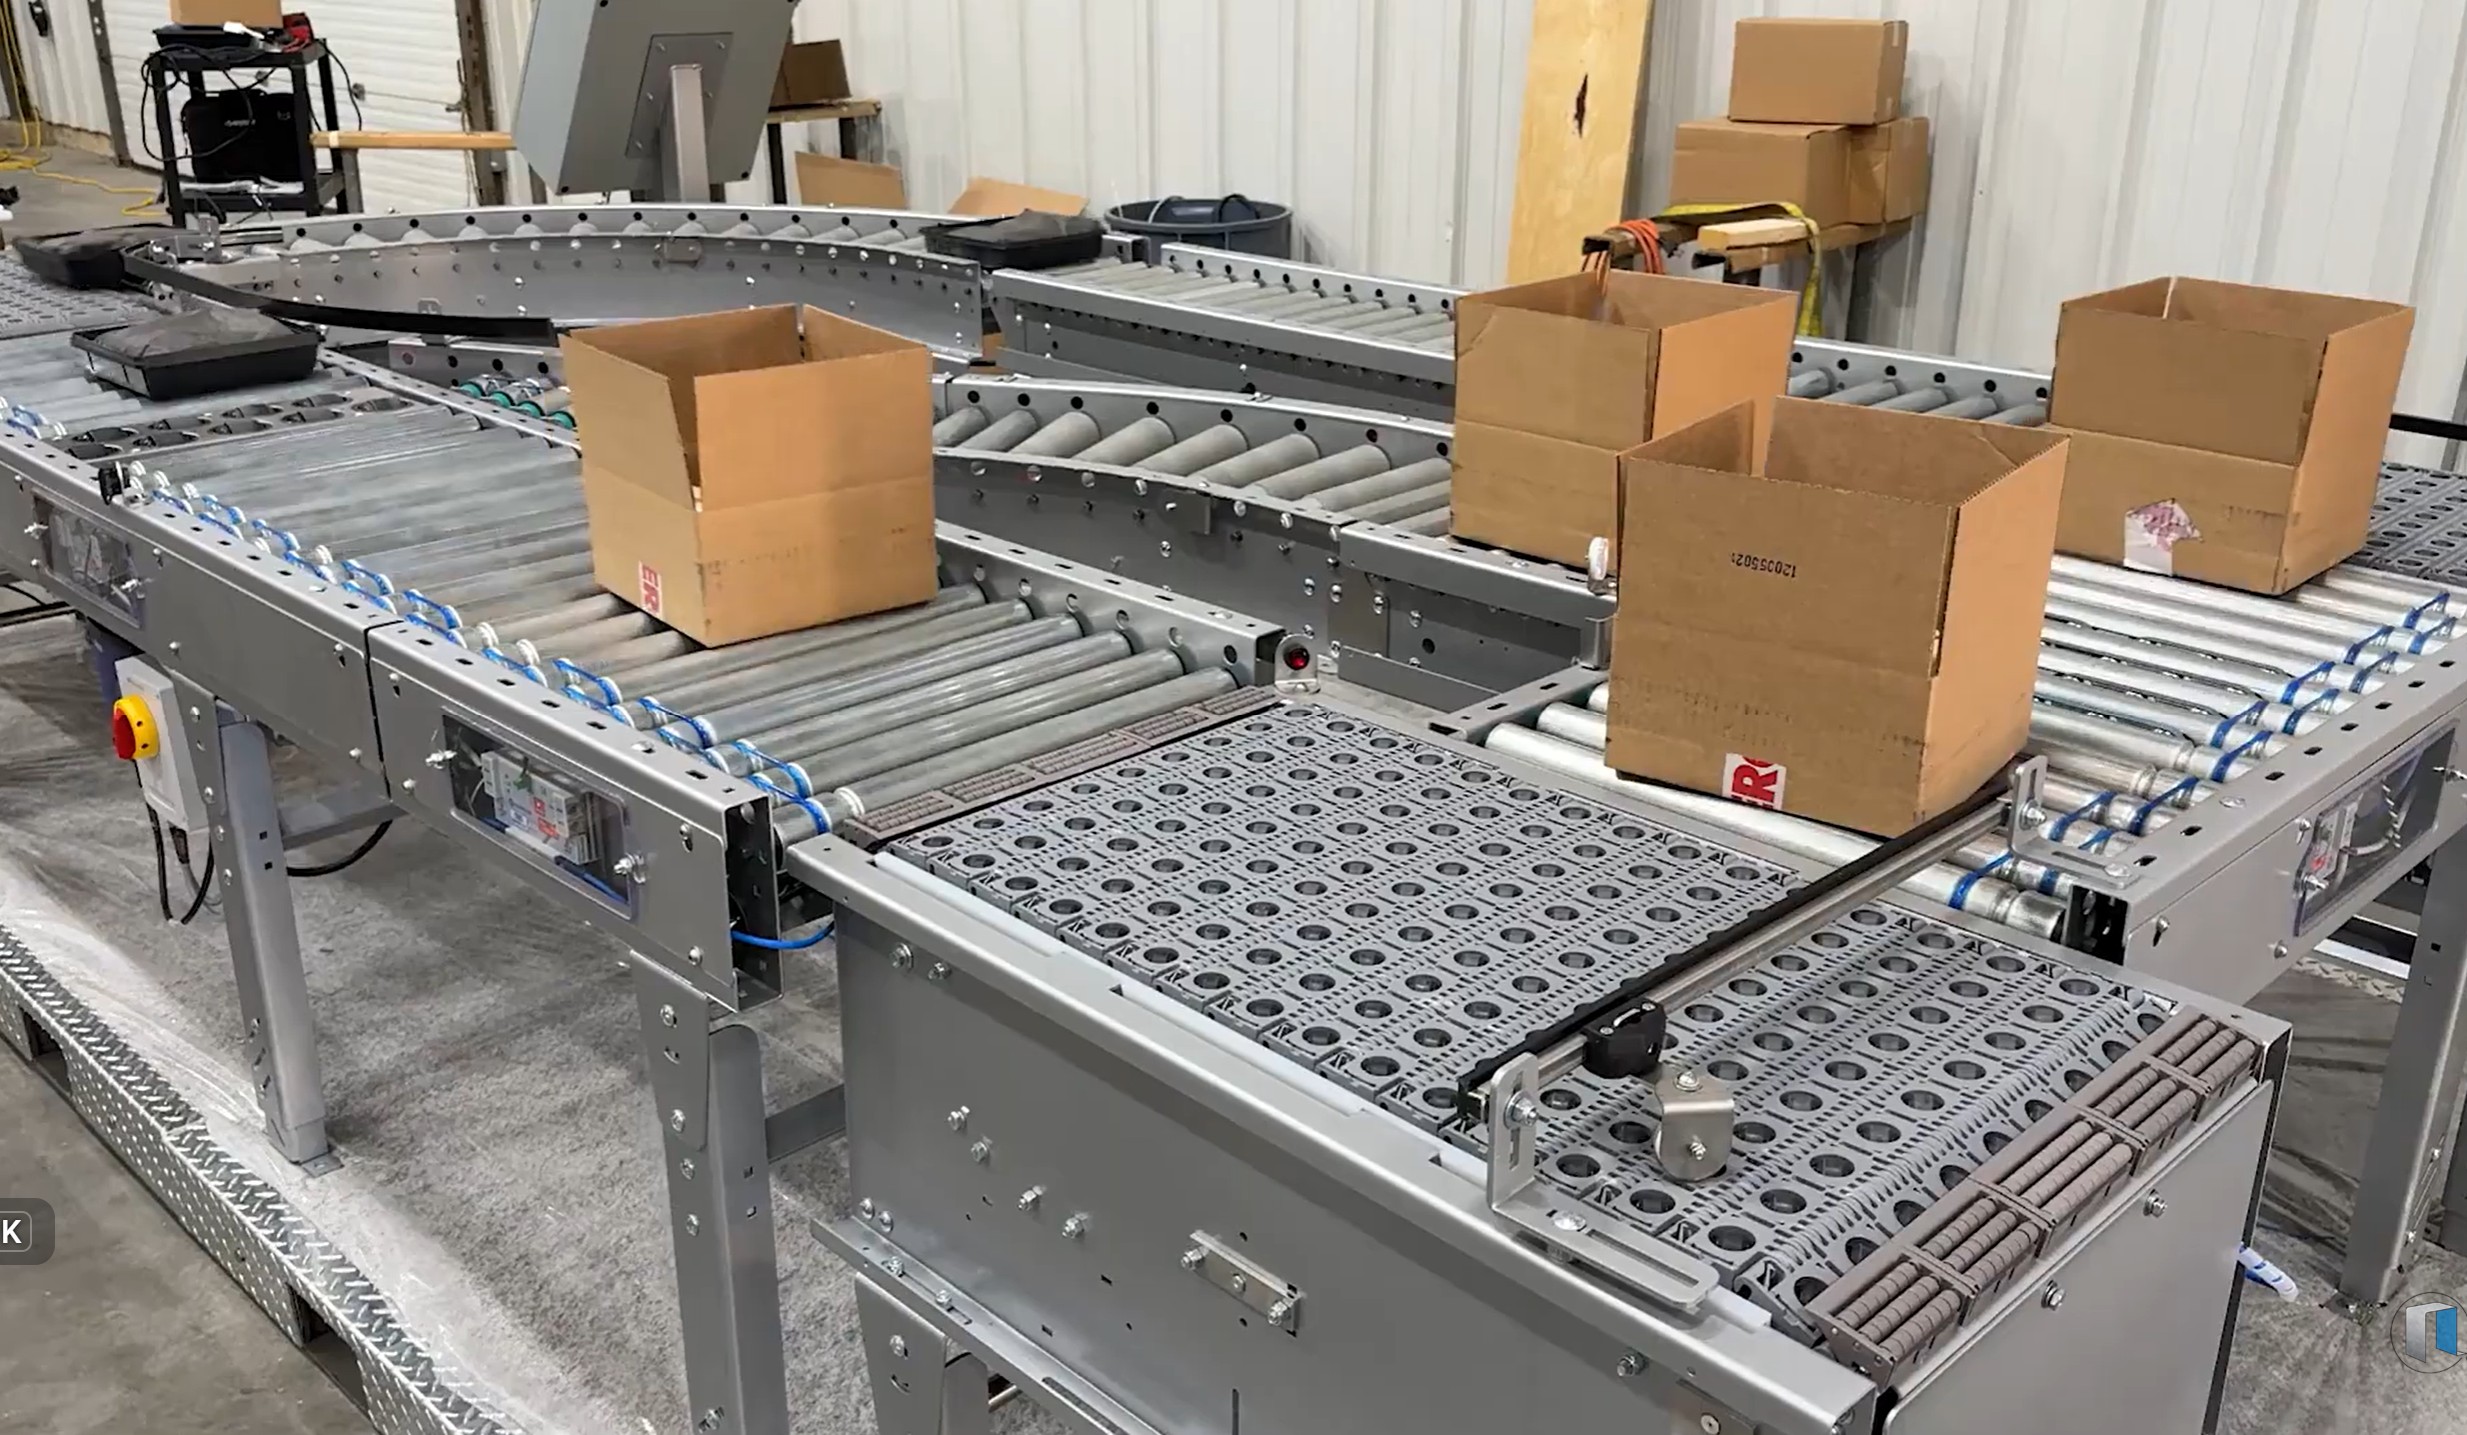
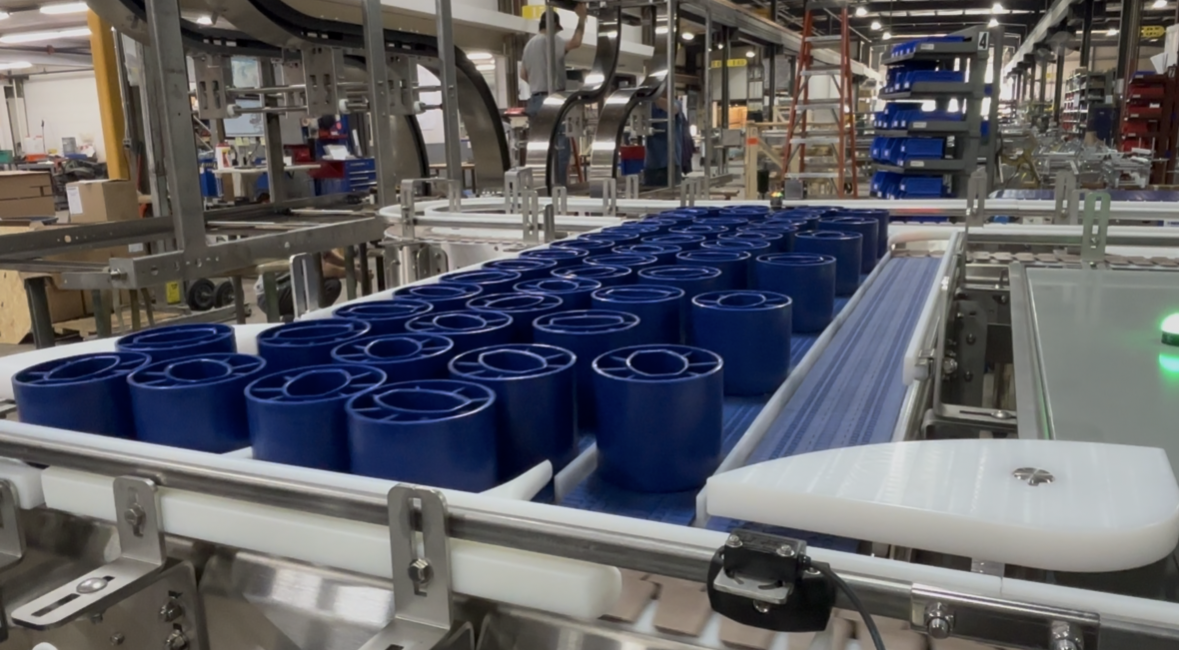
Motor Driven Roller Conveyor expands Nercon’s conveyor offering for carton, tray, and case handling applications. MDR uses individually powered roller zones to transport, accumulate, merge, divert, align, and reject products with fewer external devices such as clamps, pushers, overhead diverters, or stops.
Key Features
-
Standard Widths: 15", 21", 27", 33"
-
Zone Lengths: 15”, 18”, 21”, 24”, 27”, *30” (*Best cost value) 3” Roller centers
-
Speed: 10.8 FPM to 107.5 FPM
-
Turns: 15°, 30°, 45°, 60°, 90°
-
Product Size: Min 4” x 9” (direction of flow), Max length 30”
-
Product Weight: Up to 50lbs with single motor.
Nercon's approach to motor driven roller conveyor creates a compact, operator-safe, lower-maintenance conveyor platform that supports Nercon's focus on flexible standard conveyor systems, custom-fit solutions, and industry-best lead times -- the result of our lean manufacturing processes.
ARB/NERCON DARB INTEGRATION:
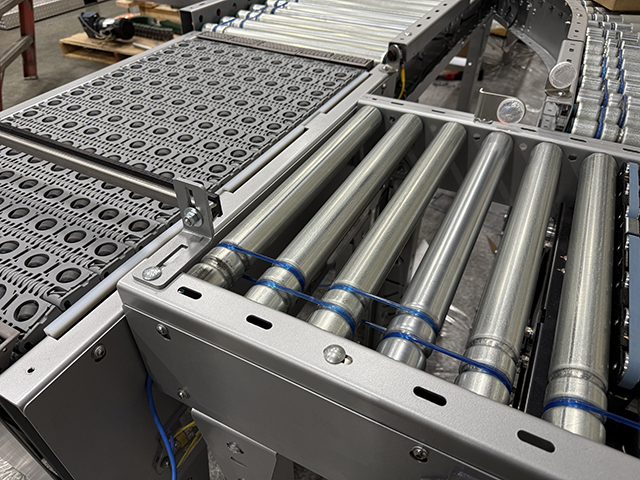
Nercon's custom integration advances ARB/DARB technology by replacing free-spinning activation rollers with a powered roller activation rack for greater control of product movement. This enables variable-angle diverts, 90-degree DARB-style transfers, and passive on/off handling in one compact module.
- DARB Transfer and Sortation
- Right Angle Transfer
- Variable Divert: 15-degrees to 75-degrees
- ARB Passive On/Off
See Our Products in Action
Watch Our Videos
Contact Us
Looking for a solution designed specifically for your needs? Share the details of your project with us, and our team will create a customized quote tailored to your goals, budget, and requirements.
Applications For Motor Driven Roller Conveyor
- Cartons
- Bundles
- Trays
- Tight Wrap
- Cases
See Our Products in Action
Explore Our Product Image Gallery
Related Industries
Beverage
Cheese & Dairy
Confectionery & Candy
Frozen Foods
Health & Beauty
Household Cleaning Products
Meat & Poultry
Pet Food & Supplies
Pharmaceuticals
Produce
Snack Food & Bakery
Request Quote
Looking for a solution designed specifically for your needs? Share the details of your project with us, and our team will create a customized quote tailored to your goals, budget, and requirements.